
How to efficiently machine shaped parts on CNC mill-turn machines?
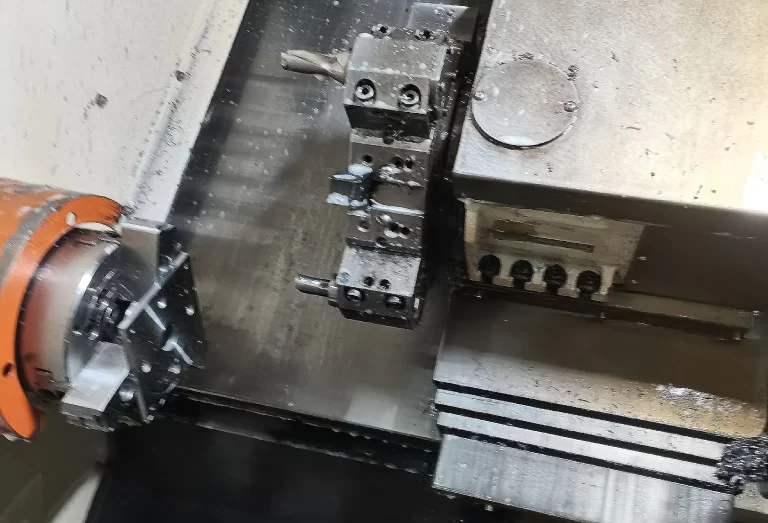

High-end manufacturing is evolving toward higher precision, efficiency, and intelligence. Precision mechanical parts are therefore being increasingly widely applied in multiple fields.
Typical application sectors mainly include the automotive and aerospace industries.
Their machining accuracy, surface quality, and production efficiency determine the performance and market competitiveness of the end products.
Turning-milling composite machining is an advanced integrated machining technology.
It integrates multiple processing functions such as turning, milling, drilling, and tapping into a unified working procedure.
This technology allows various machining operations to be finished in a single clamping setup.
By effectively reducing clamping errors and improving part machining accuracy, it has become a core technological method for the machining of precision mechanical parts.
Currently, the machinery industry faces urgent demands for energy conservation, emissions reduction, and lightweight design upgrades.
The machining accuracy standards for precision parts continue to rise in modern manufacturing industries.
Meanwhile, manufacturers need to balance mass production efficiency and cost control.
This balance is essential to accommodate the industrial transition toward large-scale production.
Nevertheless, most enterprises encounter various bottlenecks in the composite turning and milling of precision mechanical parts.
They have not established standardized and systematic process routes. We find that their machining operations adopt unreasonable sequences.
These problems further lead to redundant machining procedures and excessive idle waiting time.
Cutting parameters are set based on the operator’s experience rather than taking into account the part’s material, machining characteristics, and equipment performance;
Tool and fixture configurations are unreasonable, resulting in poor versatility and insufficient positioning accuracy;
The equipment operation and maintenance system is inadequate, leading to high rates of downtime due to malfunctions;
The level of digital management and control is low, preventing the real-time collection and analysis of machining process data.
Based on practical experience in the combined turning and milling of precision mechanical components, this paper conducts a multidimensional and systematic study on process optimization.
The aim is to resolve machining bottlenecks, improve machining accuracy and production efficiency, reduce production costs, and provide practical guidance for the machining of similar parts.
Turn-mill composite machining integrates the core components of a turning spindle and a milling power head onto a single machine tool.
It enables the completion of multiple machining operations—including turning outer diameters, inner bores, end faces, and threads, as well as milling flat surfaces, grooves, and curved surfaces—in a single setup.
The centralization of these operations is its core characteristic. This technology outperforms traditional multi-step machining methods in multiple aspects.
It greatly reduces the repeated setup of workpieces and avoids the accumulation of clamping errors.
It effectively enhances the dimensional accuracy and geometric tolerance control of machined parts.
In addition, it cuts down the time consumed by part transfer and idle waiting.
The proposed method significantly improves the overall production efficiency.
Multiple factors jointly affect the quality and efficiency of turning-milling composite machining.
These factors cover machining processes and cutting parameters.
They also include tool performance, fixture positioning accuracy, and equipment operating stability.
In addition, the professional proficiency of operators serves as a key influential factor.
Among these, the rational planning of the machining sequence serves as the foundation; the scientific setting of cutting parameters is the key;
And the compatibility of tools and fixtures is a crucial guarantee of machining quality.
These three elements work in concert and complement one another, collectively determining the overall machining outcome.
In China, the combined turning and milling field for precision mechanical parts features advanced technical capabilities but suffers from insufficient standardization in practical applications.
Most enterprises possess advanced high-end machining equipment.
They have established solid hardware foundations to support high-precision and high-efficiency machining.
However, these enterprises still have prominent deficiencies in supporting software technologies.
These weak links mainly involve process planning, parameter configuration, as well as equipment operation and maintenance management.
As a result, the equipment’s full potential remains untapped, and both machining quality and production efficiency fall short of expectations.
We summarize the core issues into the following five aspects.
Process route planning lacks rationality.
Many enterprises still adopt conventional machining processes in actual production.
They cannot fully exploit the technical advantages of turning-milling composite machining.
This situation leads to poor process coordination and redundant machining procedures, accompanied by long idle waiting time.
Moreover, the process design fails to fully consider key practical issues such as workpiece deformation and insufficient stress relief.
These inadequate design considerations ultimately degrade the overall machining quality of parts.
Cutting parameter settings lack scientific rigor.
Operators often determine cutting parameters based on their experience; they may overemphasize machining quality, which reduces machining efficiency and raises production costs.
Furthermore, the pursuit of machining efficiency can lead to excessive cutting forces, resulting in problems such as part deformation and rapid tool wear.
Inadequate tool and fixture configuration.
Tool selection does not take into account the material and structural characteristics of the parts, and poor tool management leads to excessive tool wear.
Fixtures suffer from issues such as low positioning accuracy and poor versatility, which not only prolong setup times but also increase machining costs.
The level of equipment operation, maintenance, and control urgently needs improvement.
Many enterprises experience high rates of equipment downtime due to failures;
A lack of routine operation and maintenance leads to accelerated wear of critical components, which affects machining accuracy.
Furthermore, the machining process lacks digital control and monitoring.
Operators cannot monitor or analyze relevant data, which restricts product quality and production progress.
Operators lack sufficient professional skills. Some personnel have not received specialized training in turning-milling composite machining and lack knowledge of process optimization and machining principles.
Consequently, they are unable to effectively handle machining anomalies, which in turn affects machining quality and efficiency.
To address the aforementioned issues, drawing on practical experience in the machining of precision parts for internal combustion engine components, this paper uses internal combustion engine parts as an example.
This study carries out analysis from five key research dimensions.
These dimensions include machining process sequences, cutting parameters, tool and fixture configuration, equipment operation and maintenance, as well as digital monitoring and control.
On this basis, a systematic process optimization plan is formulated.
The proposed plan can effectively improve both the machining accuracy and production efficiency.
The core of process route optimization is to fully leverage the advantages of centralized turning-milling composite operations.
This research follows several core machining principles. It strictly separates roughing and finishing processes, arranges reasonable process sequence transitions, minimizes workpiece setups, and effectively avoids machining deformation.
Meanwhile, it fully considers the structural machining characteristics of parts and the inherent properties of machining materials.
Through process integration, stress relief treatment, and sequence optimization, we significantly shorten the machining cycle and effectively improve the overall machining accuracy.
Process integration and simplification rely on the inherent advantages of turning-milling composite equipment.
We integrate multiple independent traditional machining procedures and complete them on a single machine tool.
This manufacturing mode supports diverse machining operations within one-time clamping.
It effectively reduces the total number of workpiece setups and shortens the single-piece machining cycle.
We illustrate the optimization effect by taking the machining of internal combustion engine connecting rods as an example.
The traditional machining scheme requires five separate workpiece setups.
After process optimization, we complete the entire machining procedure with only one single setup.
This optimized process supports end-face turning, drilling, and turning of large and small ends in one clamping state.
The fine grinding of both end faces is subsequently conducted as an independent finishing process.
We reduce the number of setups from five to two, thereby improving machining efficiency.
Separating roughing from finishing and incorporating stress relief are necessary to address stress-induced deformation in parts.
We schedule roughing and finishing separately and add a stress relief process after roughing.
Natural aging is the preferred method, as it effectively releases internal stresses and reduces part deformation.
A typical example is the machining of high-precision valve seat rings for internal combustion engines.
We perform low-temperature annealing treatment immediately after the rough machining process.
This treatment effectively improves the precision control of form and position tolerance errors during the subsequent finishing machining stage.
Optimizing the process sequence requires tailoring the sequence to the specific machining characteristics of the part.
We schedule operations such as drilling and tapping after turning and milling to prevent metal chips from scratching already machined surfaces.
We arrange finishing operations during periods when the equipment runs stably to minimize the impact of vibrations during startup.
A “from the inside out” and “from rough to finish” sequence is adopted for parts with multiple steps and grooves to minimize interference.
We machine circumferential rectangular keyways using an intermittent, staggered approach to avoid thermal stress concentration or deformation.
This study adopts a combined research method of theoretical analysis and process testing.
It fully considers the workpiece material properties, machining characteristics, and machine tool performance.
Following the principles of accuracy priority, efficiency balance, and controllable cost, we optimize three key cutting parameters, including spindle speed, feed rate, and cutting depth, and finally determine the optimal combination of process parameters.
We conduct theoretical analysis to preliminarily determine the relevant parameters.
Based on metal-cutting theory, excessively high spindle speeds accelerate tool wear; excessively fast feed rates can easily cause part deformation;
And excessive cutting depths compromise machining accuracy.
Combining the mechanical properties of the part with equipment parameters, we must establish a preliminary range of cutting parameters.
We carry out process trials to determine the parameters.
This study takes 45 steel precision shaft parts as the research object.
A single-factor experimental method is adopted for parameter exploration.
We conduct machining experiments using a turning-milling machining center and carbide-coated cutting tools, and deploy a coordinate measuring machine (CMM) and other testing equipment for data acquisition.
We measure multiple evaluation indicators under different parameter combinations, including machining accuracy, surface roughness, tool wear, and single-piece processing time.
The optimal parameter combination is then determined through orthogonal experimental design analysis.
At the same time, different parameters are set for rough machining, semi-finishing, and finishing.
Rough machining aims for efficient material removal and employs a large cutting depth along with moderate feed rates and spindle speeds;
Semi-finishing eliminates residual errors from rough machining and uses moderate parameters;
Finishing ensures precision and surface quality, employing small cutting depths and feed rates, along with moderate spindle speeds.
This optimization scheme complies with the procedural requirements of turning-milling composite machining and adapts to the unique machining characteristics of workpiece parts.
Optimizations are conducted in three core aspects: cutting tool selection, tool management, and fixture design.
These targeted improvements boost workpiece positioning accuracy and clamping efficiency.
Additionally, they mitigate tool wear and effectively reduce overall manufacturing costs.
For cutting tool selection and parameter optimization, we select appropriate tools according to the part material and machining characteristics.
Common steels such as 45 steel are machined using YT15 and YW2 carbide-coated cutting tools because of their high hardness and excellent wear resistance.
For machining high-strength and high-hardness parts, we recommend ceramic or cubic boron nitride (CBN) cutting tools.
At the same time, based on the part’s machining characteristics, it is necessary to appropriately select solid, modular, or specialized form tools, and optimize geometric parameters such as the rake angle and clearance angle to ensure machining quality.
It is essential to improve the tool management system and mechanisms, ensuring proper classification and labeling of tools during warehousing and inventory management to achieve full traceability throughout the tool lifecycle.
Use online monitoring equipment to track tool wear in real time, providing timely alerts for replacement when wear reaches critical thresholds to prevent any impact on machining quality.
We can reuse slightly worn tools after regrinding to improve tool utilization.
Periodically analyze tool consumption data to optimize tool selection and cutting parameters, thereby achieving cost control.
Establish a standardized tool library to pre-match tools with corresponding cutting parameters, effectively reducing tool changeover time and improving machining efficiency.
Fixture design and optimization must focus on precision, versatility, and stability.
Design high-precision, versatile, specialized fixtures that utilize high-precision positioning methods—such as “one face, two pins” and zero-point positioning systems—to strictly control positioning errors within permissible limits;
Develop flexible fixtures to accommodate parts of different specifications, reduce the frequency of fixture changes, and lower the costs associated with setup time.
We adopt standardized clamping methods, including hydraulic and pneumatic systems, in the machining process.
These systems deliver stable and uniform clamping force during workpiece fixation.
This approach avoids part deformation induced by excessive clamping load.
Accordingly, we effectively guarantee the overall machining accuracy of workpieces.
This study fully considers the structural characteristics and standardized operating specifications of mill-turn machining centers.
We establish a scientific and comprehensive system for equipment operation and maintenance.
This system focuses on reducing equipment failure and downtime caused by malfunctions.
It effectively sustains stable machining accuracy and extends the service life of machining equipment.
We have established a robust preventive maintenance mechanism, moving away from the traditional reactive maintenance model, and developed detailed, actionable maintenance plans.
For routine maintenance, operators will inspect power supplies and lubrication systems, and clean metal shavings and oil residue from the equipment.
We perform weekly inspections and maintenance on the spindle, guideways, and feed systems, conduct monthly precision testing and calibration, and carry out comprehensive maintenance and potential hazard inspections quarterly.
Define replacement cycles for wear-prone parts and replace them promptly.
At the same time, integrate automated self-test procedures so that, upon startup, the equipment automatically checks parameters such as spindle speed and feed axis accuracy to ensure it operates in optimal condition.
Strengthen equipment accuracy calibration and maintenance efforts.
Use professional testing instruments, such as laser interferometers and ball bar systems, to periodically inspect the equipment’s positioning accuracy, spindle rotation, and other precision parameters;
If deviations exceed the allowable range, adjust and calibrate the equipment promptly.
Strengthen management of the equipment operating environment by placing equipment in workshops with constant temperature and humidity and free from vibration.
Monitor environmental parameters in real time and adjust machining parameters using compensation algorithms to effectively mitigate the impact of environmental factors on equipment accuracy.
Improve the emergency response mechanism for equipment failures by establishing a professional maintenance team with clearly defined roles and responsibilities to ensure rapid response and resolution of failures.
Create an equipment failure database to meticulously record failure types, causes, and corrective actions, identify patterns in failures, and provide scientific guidance for preventive maintenance.
Develop standardized emergency response procedures for common failures to standardize operational steps and improve the efficiency of troubleshooting.
Implement remote assistance capabilities to enable real-time communication between operators and technical experts, quickly resolve equipment operation issues, and effectively reduce downtime caused by malfunctions.
It is necessary to introduce digital monitoring and control technologies and establish a comprehensive digital monitoring and control system.
Through real-time monitoring, data collection, and in-depth analysis of the machining process, production quality and progress can be precisely controlled, thereby further enhancing overall production management efficiency.
Real-Time Monitoring of the Machining Process: Sensors for cutting force, vibration, temperature, and other parameters must be installed on the equipment to monitor key machining parameters in real time.
Alerts are triggered immediately upon detecting abnormal parameters, thereby mitigating quality risks and preventing equipment failures.
Machine tools are equipped with built-in laser measurement systems or contact probes that automatically inspect key dimensions of workpieces after machining.
The inspection data is fed back to the CNC system to enable real-time parameter compensation, ensuring machining accuracy.
At the same time, the integration of AI vision inspection technology enables rapid identification of surface defects on workpieces, with both inspection speed and accuracy surpassing those of traditional manual inspection.
For the data collection and analysis phase, a machining process data collection system must be established to collect parameters such as equipment operating status, machining quality indicators, and production progress in real time.
Centralized storage ensures full traceability of data throughout the entire process.
Specialized data analysis software is introduced to unlock the value of the data, providing a scientific basis for process optimization, equipment operation and maintenance, and production management.
A digital twin model is constructed to enable data traceability throughout the entire machining lifecycle.
The system can automatically generate visual production reports that intuitively present various production data, providing reliable data support for production optimization decisions.
Optimizing production planning and scheduling requires using digitally managed data as the core basis.
By integrating order requirements, equipment operating status, and process standards, scientific production plans are formulated, clearly defining the specific tasks and progress milestones for each piece of equipment and each production step.
Production scheduling management software is applied to realize real-time monitoring of the entire production progress.
Once abnormal conditions occur, including equipment failures and unqualified product quality, production plans and scheduling strategies can be adjusted promptly.
This effective intervention guarantees the stable operation of the production process and avoids unexpected production shutdowns.
To validate the feasibility and effectiveness of the process optimization scheme proposed in this paper, precision shaft components made of 45 steel from a certain internal combustion engine parts manufacturer were selected as test subjects.
Comparative tests were conducted before and after optimization to measure and analyze key indicators such as machining accuracy, production efficiency, and production costs.
The CKX6140 turning and milling machining center was selected as the test equipment, and the test parts were precision shaft components made of 45 steel.
Before tool optimization, standard YT15 carbide tools were used;
After optimization, YT15-coated tools were used.
For clamping, a standard three-jaw chuck was used before optimization, while a high-precision flexible fixture was used after optimization.
The selected measuring instruments included a coordinate measuring machine (CMM), a surface roughness tester, and a tool wear measuring instrument.
A total of 100 parts of each type were machined to compare the machining parameters before and after optimization.
Tables 1–3 show a comparison of part machining accuracy, production efficiency, and production costs before and after implementing the optimization plan.
As shown in the tables, part machining accuracy improved significantly after process optimization, and the machining pass rate increased substantially.
Following process optimization, production efficiency improved significantly, equipment utilization rates increased substantially, and production costs were significantly reduced.
The key reasons for these improvements are that process optimization minimized clamping errors and deformation; optimized cutting parameters reduced cutting forces and temperatures;
Optimized tools and fixtures enhanced positioning accuracy and cutting performance; and equipment operation, maintenance, and control ensured machining stability.
Implementation Status | Dimensional Error (mm) | Geometric Tolerance (mm) | Surface Roughness (μm) | Pass Rate (%) |
|---|---|---|---|---|
Before Implementation | 0.007–0.010 | 0.008–0.012 | 1.0–1.6 | 89.2 |
After Implementation | 0.004–0.006 | 0.005–0.008 | 0.6–0.9 | 95.7 |
Table 1. Comparison of Part Machining Accuracy
Implementation Status | Machining Time per Part (min) | Production Output (parts/h) | Equipment Utilization Rate (%) |
|---|---|---|---|
Before Implementation | 12.3 | 4.9 | 78.5 |
After Implementation | 9.8 | 6.1 | 91.3 |
Tab 2. Comparison of Production Efficiency
Implementation Status | Labor | Tool Consumption | Equipment Energy Consumption | Scrap Loss | Total |
|---|---|---|---|---|---|
Before Implementation | 1,250 | 850 | 625 | 320 | 3,045 |
After Implementation | 960 | 680 | 580 | 99 | 2,319 |
Table 3. Comparison of Production Costs (CNY)
Based on actual production practices in the combined turning and milling of precision mechanical parts, this paper conducts a systematic study on process optimization to address various core issues encountered during machining.
After practical validation, it was ultimately concluded that the multidimensional, systematic process optimization scheme proposed in this paper is highly feasible and effective.
It can significantly improve the machining accuracy and production efficiency of precision mechanical parts, effectively reduce production costs, and overcome the current bottlenecks in the turning-milling composite machining process.
This optimization scheme is suitable for the batch production of precision parts and also provides practical experience that can be applied to the machining of similar precision parts, thereby holding significant engineering value.
With the rapid development of the modern manufacturing industry, the…
Easy to deform thin-walled parts processing, has been the processing…
Now we attach importance to the design of intelligent agricultural…